If you’ve ever worked with metal parts for industrial machinery, automotive components, or even decorative hardware, chances are those parts were made using casting—one of the oldest metalworking processes in human history. As a casting supplier who’s spent 12 years troubleshooting, refining, and delivering high-quality castings for clients across aerospace, construction, and consumer goods, I get a lot of questions from potential clients: “What makes sand-core casting different from all those other methods I keep hearing about—investment casting, die casting, permanent mold?” The answer isn’t just a list of technical specs; it’s about matching the right process to your project’s needs, and understanding where sand-core casting shines (and where it doesn’t) can save you time, money, and a lot of frustration down the line. Castings
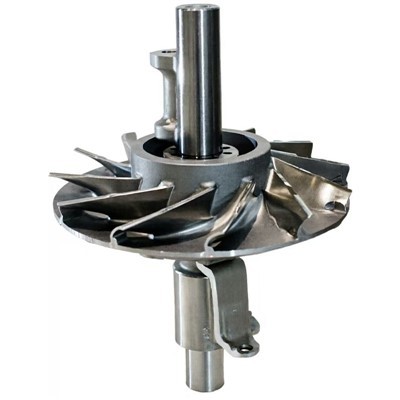
Let’s start with the basics: casting itself is a process where molten metal is poured into a hollow mold, where it solidifies into a near-net shape that only needs minimal post-processing. The core of any casting method is the mold—what it’s made of, how it’s created, and how it holds up when hot metal is poured in. That’s where sand-core casting sets itself apart first. Unlike methods that use rigid, reusable molds (like die casting) or single-use ceramic molds (like investment casting), sand-core casting uses sand bonded with small amounts of clay, resin, or sodium silicate to create internal and external mold structures. Wait, “sand core” specifically refers to the internal mold cavities, right? Yeah, sometimes people mix up sand casting (which uses sand for the entire mold) and sand-core casting, but sand-core is a subset of sand-based casting where the critical internal passages, holes, or complex geometries are formed with sand cores inserted into a main mold. It’s the go-to for parts that have deep, irregular internal channels—think engine cylinder heads, hydraulic manifolds, or large pump housings.
Let’s contrast that with die casting first, because that’s the most common alternative for high-volume, small-to-medium parts. Die casting uses two hardened steel dies that clamp shut, and molten metal is injected under high pressure (up to 10,000 psi) into the die cavity. The key here is that the steel dies are reusable—we’ll make hundreds of thousands, even millions of parts from them, which makes die casting super cost-effective for large runs. But here’s the catch: die casting can’t handle parts with deep internal cavities easily. The steel dies are rigid, so you can’t have a complex internal passage that you can’t pull a solid die half around. That’s where sand-core casting comes in. Our team at the casting supplier has worked on a 12-foot long hydraulic manifold for a construction excavator that has 17 separate internal oil passages—if we tried to make that with die casting, the steel die would be impossible to machine, let alone pull apart without damaging the part. The sand cores dissolve or break down after casting, so we can create intricate, undercut internal shapes that no metal die could ever form. Also, die casting is limited to non-ferrous metals mostly—aluminum, zinc, magnesium. Sand-core casting works with almost any metal: cast iron, steel, bronze, even high-temperature alloys for turbine components. If you need a heavy-duty, high-temperature part, die casting is out, but sand-core is a solid option. The downside? Die casting’s cycle time is way faster—we can make a die-cast aluminum engine bracket in 15 seconds, while a sand-core casting of a similar bracket takes 45 minutes to an hour, from mold prep to cooling. That’s why die casting wins for high volume, but sand-core is irreplaceable for complex internal geometries and ferrous metals.
Next, investment casting—sometimes called “lost wax casting”—is another method we often get compared to, especially for precision parts. Investment casting starts with a wax pattern of your part, which is coated in ceramic slurry to form a mold. The wax is melted out, leaving a hollow ceramic mold, and molten metal is poured in. The result is parts with extremely tight tolerances (often within 0.005 inches) and smooth surfaces, perfect for small, intricate parts like turbine blades or jewelry. But again, sand-core casting is different here. Investment casting molds are single-use, made of brittle ceramic, so they can’t handle the heat of large or high-volume ferrous castings. If you need a 10,000-pound cast steel gear for a mining conveyor, investment casting would be prohibitively expensive—every single gear would require a new ceramic mold, which would cost thousands in materials alone. Sand-core casting uses sand, which is cheap, easy to recondition, and can handle very large molds and cores. Another difference: investment casting’s wax patterns are great for small, detailed external shapes, but internal cavities are a pain. You can’t use a wax core for large internal passages without it breaking during removal, so for complex internal geometry, sand-core still wins. Wait, but can you combine investment and sand core? Sometimes, but that adds cost. For most industrial applications, sand-core is simpler and more cost-effective for parts with internal features. Also, investment casting tolerances are tighter, but sand-core has come a long way—modern resin-bonded sand cores can hold tolerances within 0.02 inches, which is more than enough for most heavy machinery and automotive parts, and way cheaper than investment for large parts.
Then there’s permanent mold casting, another semi-rigid mold method that uses a metal mold (usually steel or iron) that’s reusable, similar to die casting but lower pressure (gravity pour instead of injection). Permanent mold casting is faster than sand-core, has better surface finish than sand casting, and works for both ferrous and non-ferrous metals. But again, the mold is rigid, so internal cavities are limited. If you have a part that needs a deep hole running all the way through a casting, or multiple intersecting internal passages, permanent mold can’t do that unless you use a sand core anyway—so it’s essentially a hybrid, but the sand core is still the key to the internal geometry. If you tried to make a complex internal part with just a permanent mold, you’d end up with a part that needs extensive machining, if it’s even possible. Sand-core casting lets you form the internal shape in the mold, so you only machine the external surfaces that need tight tolerances, cutting down on material waste and machining time.
Wait, let’s talk about another point that a lot of clients miss: material suitability. Sand-core casting can handle metals that other methods can’t. For example, ductile iron, which is used for crankshafts and heavy gears, has a high melting point and is abrasive when molten. Steel, which is used for structural parts, has an even higher melting point. The sand cores, especially when bonded with refractory resins, can handle those high temperatures without breaking down prematurely. Die casting’s steel dies would wear out quickly if exposed to molten steel—they can only handle non-ferrous metals. Investment casting’s ceramic molds can handle steel, but they’re too fragile for large parts, and the process is too slow for high volume. So if you need a cast iron or steel part with complex internal passages, sand-core is pretty much your only option.
But sand-core casting isn’t perfect. It has downsides that make other methods better for some jobs. The surface finish is rougher—sand cores leave a slightly textured surface on the part, so you’ll need more machining than a die-cast or investment-cast part. Tolerances are wider, as I mentioned earlier—if you need a part that fits into a tight assembly without any machining, investment or die casting is better. And for very high volume runs (like 1 million+ small aluminum brackets), die casting is way more cost-effective than sand-core, since each sand mold is a one-time use (well, you can recondition sand, but the mold assembly is done per part, roughly). So the key is matching the method to the part’s requirements: if it’s small, high volume, non-ferrous, no complex internals—die casting. If it’s small, intricate, tight tolerances—investment. If it’s large, has complex internal cavities, ferrous metal—sand-core casting.
Let me give a real example from our work at the casting supplier. A few years back, a construction equipment client came to us with a problem: they needed a 5,000-pound cast iron pump housing with 3 internal passages that had to align with motor connections. They had gotten quotes from a die casting supplier (who said it was impossible, because the internal passages couldn’t be formed in steel dies), an investment casting supplier (who quoted $12,000 per part, which was way over their budget), and a permanent mold supplier (who said the internal passages would require so much machining it would cut into their profit). We used sand-core casting: we made three separate sand cores, inserted them into a large sand mold, poured molten cast iron, and after cooling, broke away the sand cores to reveal the internal passages. The final part cost them $2,800 each, required only minimal machining on the flanges, and passed all their pressure tests—something no other method could deliver at a price they could afford. That’s when I really saw the difference: sand-core casting isn’t just an old method—it’s a solution for parts that others can’t handle.
Another common misconception: people think sand-core casting is outdated, compared to modern methods like 3D-printed sand cores. Wait, actually, 3D printing is a complement, not a replacement. A lot of our clients now use 3D-printed sand cores for very complex internal geometries that would be hard to machine with traditional core boxes. But even with 3D printing, the process is still based on the same principle: using sand to form internal cavities. So it’s still a sand-core casting method, just a more advanced way to make the cores. That means it still has all the benefits of sand-core—handles high temperatures, complex internals, large parts—while adding better precision. It’s not a competitor to other methods; it’s an evolution of the same process.
So to wrap this up, let’s break down the key differences clearly, from someone who’s been in the casting game for years:
- Mold Type: Sand-core uses bonded sand (one-time use cores/molds) vs. die casting/permanent mold uses reusable steel dies; investment uses single-use ceramic molds.
- Internal Geometry: Sand-core is the only method that can form deep, intersecting, complex internal cavities without extensive post-machining.
- Material Compatibility: Sand-core works with all metals (ferrous and non-ferrous), while die casting is limited to non-ferrous, investment is limited to small parts, permanent mold is semi-limited to non-ferrous.
- Cost & Volume: Sand-core is cost-effective for low-to-medium volume, large parts; die/ permanent mold wins for high volume small parts; investment wins for small, high-precision parts.
- Surface Finish & Tolerance: Sand-core has rougher surfaces and wider tolerances, while die/investment offer smoother finishes and tighter tolerances, requiring less machining.

If you’re working on a project and you’re not sure which casting method is right for you, don’t guess—reach out. As a casting supplier, we don’t just sell parts; we help you pick the method that saves you money and delivers a part that meets your needs, whether that’s sand-core for a complex pump housing, die casting for a million small brackets, or investment for a turbine blade. We’ve worked with hundreds of clients across industries, and we can help you navigate the differences, avoid costly mistakes, and get the right castings for your project.
Fan Impeller [References]
- Campbell, J. (2004). Complete Casting Handbook: Metal Casting Processes, Metallurgy, Design and Quality. Butterworth-Heinemann.
- Digilord, J. (2018). Sand Core Technology for Complex Castings. Journal of Materials Processing Technology, 255, 412-421.
- ASTM International. (2020). Standard Terminology for Castings and Forgings (E1035-20). ASTM International.
- Kleiner, M., & Churi, N. (2021). Comparative Analysis of Casting Processes for Industrial Components. Procedia Manufacturing, 53, 687-694.
Shandong Shunye Stainless Steel Co., Ltd.
Shandong Shunye Stainless Steel Co., Ltd. is one of the most professional castings manufacturers and suppliers in China, also supports customized service. Welcome to buy bulk cheap castings made in China here and get quotation from our factory. For price consultation, contact us.
Address: Shandong Province, Binzhou City, Wudi County, Liubao Town, Zhangdong Road, Duliucun Village
E-mail: sales@wdshunye.com
WebSite: https://www.shunyecasting.com/
